A failed dielectric test after a harness, actuator, power unit, or avionics assembly has reached final integration is rarely just a test failure. It can indicate an unclear insulation requirement, an unsuitable fixture, an unrepresentative voltage profile, or test data that cannot support a disposition decision. Effective aerospace dielectric test planning addresses those issues before the unit reaches the test station.
For aerospace programs, dielectric withstand testing is not a generic pass/fail activity. The plan must connect the product’s insulation system, operating environment, governing specification, test stage, and measurement method. That connection protects personnel and equipment while producing evidence that engineering, quality, and certification teams can defend.
Start With the Requirement, Not the Tester
The first planning task is to identify the exact requirement that applies to the assembly under test. This may come from an aircraft or spacecraft platform specification, a customer drawing, an internal engineering standard, or an applicable industry standard. The governing document should establish the test voltage, waveform, duration, allowable leakage current, test points, environmental condition, and acceptance criteria.
Requirements often differ substantially between component qualification and production screening. A qualification test may include elevated voltage margins, extended dwell times, temperature exposure, humidity conditioning, altitude considerations, or repeated stress cycles. A production test is usually designed to verify workmanship and insulation integrity without imposing unnecessary cumulative stress on every delivered unit.
That distinction matters. Applying a qualification-level test indiscriminately on the production line can damage marginal insulation systems or reduce long-term reliability. Conversely, reducing a specified qualification test to improve throughput can leave a critical failure mode unexamined. The correct test profile depends on the product design and its required evidence, not simply on the voltage capability of the available instrument.
The plan should explicitly document whether the test is AC withstand, DC withstand, insulation resistance, or a coordinated sequence using more than one method. AC testing can expose dielectric loss and capacitive effects that a DC test may not reveal. DC testing can offer more controlled leakage-current interpretation after capacitive charging has settled. Neither method is universally better. The appropriate choice follows the applicable requirement and the electrical behavior of the unit under test.
Define the Unit Under Test and Electrical Boundaries
Aerospace electrical assemblies are rarely simple two-terminal devices. A cable harness can include shields, multiple conductor groups, backshells, connector shells, splices, and components with different voltage ratings. An integrated power assembly may include sensitive control electronics, filters, contactors, transformers, and intentional paths to chassis.
Before a test program is released, engineering should define each test connection and every point that must be isolated, shorted, grounded, or excluded. A test-point matrix is often more useful than a single wiring diagram because it records the source connection, return connection, voltage level, dwell time, current limit, and required configuration for each test.
This is where avoidable failures often originate. A shield that should be isolated may be bonded to return. A surge protection device may begin conducting at the planned test voltage. Parallel circuits may create a normal leakage path that looks like insulation breakdown. A previously unconsidered capacitive load may cause a current transient that exceeds an overly tight limit during ramp-up.
The plan should identify these expected electrical behaviors in advance. Acceptance limits should distinguish charging current, steady-state leakage, and true breakdown behavior where the instrument and procedure support that distinction. If a design requires temporary jumpers or removal of sensitive subassemblies, those actions need controlled work instructions and configuration verification.
Consider the Environment the Insulation Will See
Aerospace insulation performance is affected by more than nominal bus voltage. Pressure, humidity, contamination, vibration, temperature cycling, and altitude can all alter dielectric behavior. Partial discharge risk can be especially relevant in high-altitude applications, where reduced air density changes breakdown conditions.
Not every production dielectric test must replicate the operating environment. However, the planning process should establish which environmental stresses are addressed through separate qualification tests and which are verified in routine manufacturing. That separation prevents duplicated testing while preserving traceability to the program’s verification strategy.
Build a Voltage Profile That Is Controlled and Repeatable
A dielectric test voltage should be treated as a profile, not just a number. The profile includes initial voltage, ramp rate, peak voltage, dwell time, current threshold, discharge behavior, and the response to a fault. These parameters affect both defect detection and product stress.
A fast ramp can improve cycle time, but it may produce substantial capacitive charging current in long harnesses, filters, and motor windings. That current can cause nuisance trips or obscure the transition to abnormal leakage. A slower ramp can improve diagnostic clarity, though it increases station time. The right rate depends on circuit capacitance, required test method, and the capability of the test system to measure and control the event.
Current limits deserve the same attention as voltage limits. A limit set too high may permit damaging fault energy before shutdown. A limit set too low can create false failures from normal charging or leakage. Where allowed by the specification, a staged approach may help: establish a controlled ramp, allow settling, then assess leakage during the required dwell period.
The test plan should also define what happens after a trip. The system should remove high voltage promptly, discharge stored energy safely, record the measured values, and prevent automatic reapplication of voltage until the operator has completed the prescribed action. For high-capacitance assemblies, verifying discharge is a personnel safety requirement, not an administrative detail.
Engineer the Fixture as Part of the Measurement System
A test fixture is not a passive accessory. Its insulation resistance, creepage and clearance distances, connector ratings, shielding, interlocks, and grounding arrangement all influence the result. A fixture that performs adequately on a benchtop may be unsuitable for a production environment with repeated operator handling and frequent configuration changes.
Fixture design should be based on the maximum applied voltage, expected transient conditions, conductor spacing, and the physical geometry of the unit under test. It should also support error-proofing. Keyed connectors, dedicated return paths, guarded terminals where appropriate, and clear identification of test groups reduce the likelihood of a dangerous or invalid connection.
For assemblies with multiple configurations, consider a programmable switching approach rather than manual reconnection between every test point. This can improve repeatability and reduce operator exposure, but it introduces additional requirements for switching voltage ratings, leakage performance, isolation, and verification. The benefit is greatest when the switching system is qualified as part of the complete test architecture.
Safety controls must be designed into the cell. These typically include a guarded area or enclosure, door or lid interlocks, emergency stop functions, visible status indication, a safe return path, and procedures for verifying stored-energy discharge. Test managers should review the complete system behavior during a fault, not only the hipot tester’s individual specifications.
Plan for Traceable Data Before Production Begins
A passed unit with incomplete data can still create a quality problem. Aerospace programs may require serial-number traceability, test-station identification, operator credentials, software revision, fixture identification, instrument calibration status, applied voltage, leakage current, dwell time, and date-time records. The data package should be defined before the first production unit is tested.
A useful record captures both the programmed limits and the actual measured result. If a unit fails, the record should retain the failure point, measured current or voltage at trip, and test configuration. Those details support root-cause analysis and make it possible to distinguish a product defect from a fixture or setup issue.
Instrument calibration is part of measurement integrity, but calibration alone does not validate the test process. The test system should also undergo periodic functional verification using known standards or controlled artifacts appropriate to the measurement range. This confirms that the instrument, cables, fixture, switching, software, and safety circuitry work together as intended.
For automated stations, control software versions and parameter access tightly. A seemingly minor change to ramp time, leakage limit, or test sequence can affect acceptance decisions across an entire lot. Role-based access, approved test recipes, revision control, and audit-ready result storage provide practical safeguards.
Validate the Plan With Representative Samples
A released test procedure should be proven on representative product, including known-good units and, when available, controlled defect samples. This validation helps establish normal leakage ranges, charging behavior, cycle times, fixture ergonomics, and the response to intentional faults.
The goal is not merely to make the test pass. It is to confirm that the process detects the conditions it is intended to detect without creating unacceptable false rejects or product stress. If failure analysis shows that a test cannot distinguish between a benign configuration effect and insulation degradation, the answer may be a revised setup, a different test sequence, or an additional diagnostic measurement.
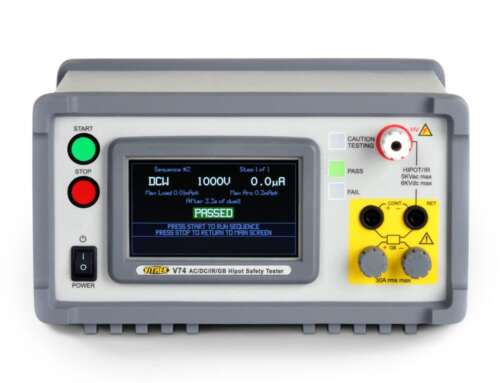
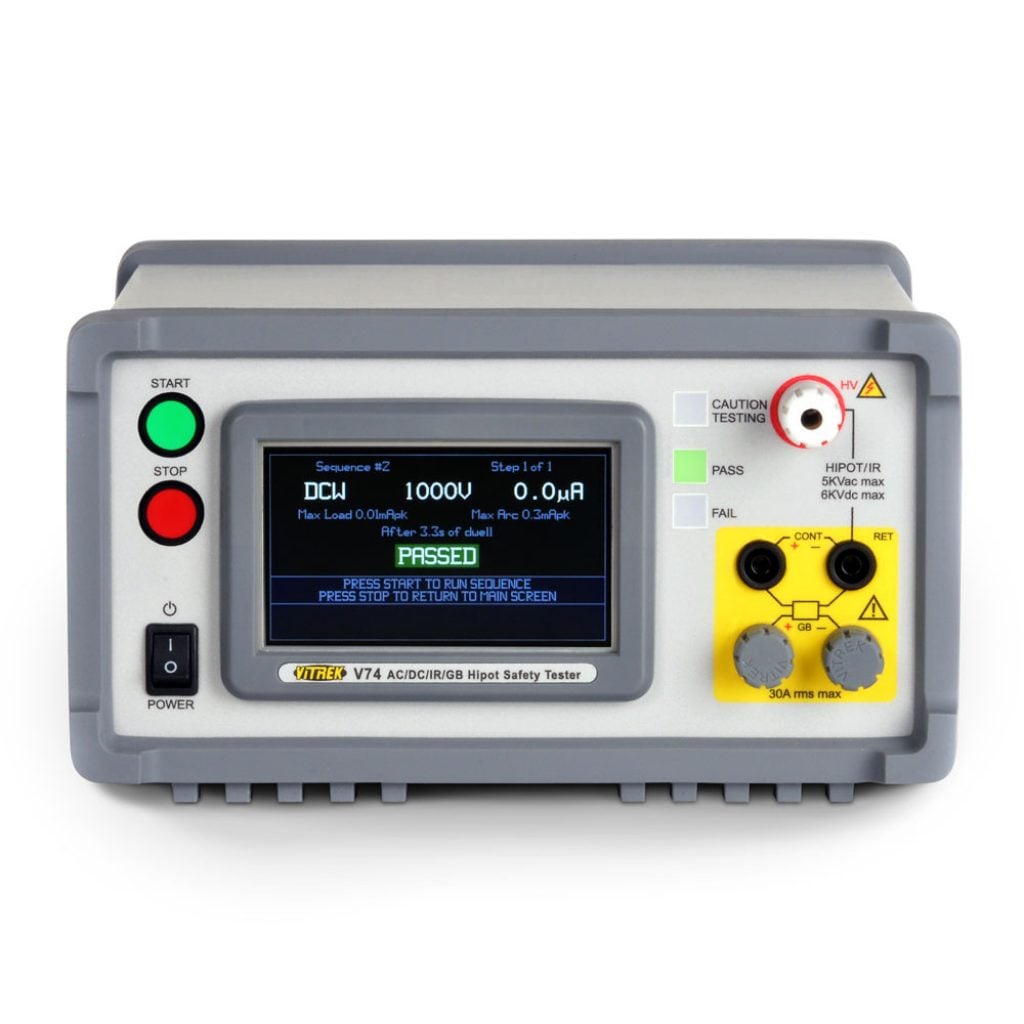
Vitrek high-voltage test systems can be configured as part of this broader approach, with controlled test profiles, automation support, and data capture matched to the requirements of the application. Selection should still begin with the test plan, including voltage range, current measurement needs, switching architecture, safety design, and traceability requirements.
Make Change Control a Test Requirement
Aerospace dielectric test planning does not end at release. Changes to wire insulation, potting material, connector supplier, assembly process, fixture wiring, software, or test instrument can alter the validity of prior assumptions. The test plan should state which changes require engineering review, correlation testing, partial revalidation, or formal requalification.
That discipline turns dielectric testing from a final inspection gate into a controlled verification process. When requirements, configurations, applied stress, safety controls, and data records remain aligned, the resulting test evidence is useful long after the unit leaves the production floor.